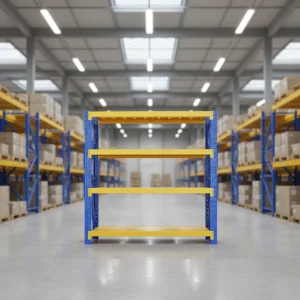
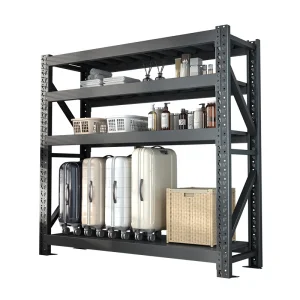
Discover our premier selection of engineered heavy-duty racks, designed for maximum load capacity, structural resilience, and seamless warehouse automation compatibility.
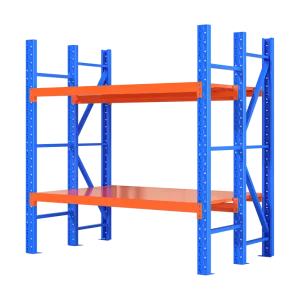
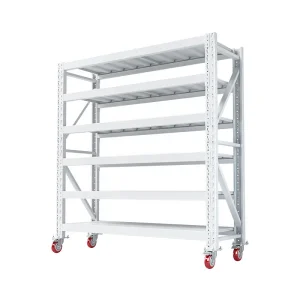
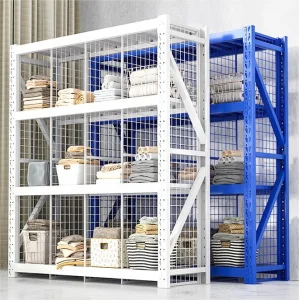
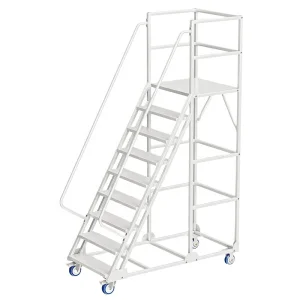
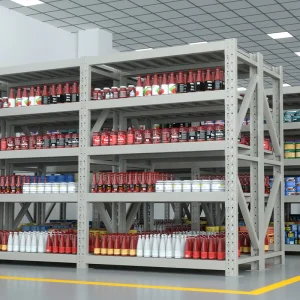
The global industrial storage and warehousing ecosystem is undergoing a massive transformation driven by rapid e-commerce expansion, omnichannel retail models, and advanced supply chain digitalization. Heavy duty racking systems serve as the physical backbone of modern logistics, empowering manufacturing plants, global distribution hubs, and third-party logistics (3PL) providers to optimize cubic storage utilization while ensuring uncompromising workplace safety.
As international trade accelerates, buyers demand certified, highly durable, and modular racking infrastructure that adapts to fluctuating SKU profiles and high-density inventory management. Strategic sourcing from verified Chinese manufacturers—backed by rigorous ISO quality frameworks, automated robotic manufacturing lines, and extensive export compliance—enables global enterprises to achieve superior operational efficiency without compromising structural integrity.
Guangdong Shibang Storage Rack Co., Ltd. was established in 2016 and is a professional manufacturer specializing in warehouse storage racks, industrial shelving systems, and customized storage solutions. With a 35,000㎡ modern production facility, we provide high-quality storage equipment for warehouses, factories, logistics centers, and commercial applications worldwide.
With an annual export revenue of approximately USD 18 million and 8 years of export experience, Shibang has accumulated 15 years of industry experience in storage rack manufacturing. Our company integrates product design, manufacturing, quality control, and global supply services to deliver reliable warehouse solutions for customers in different industries.
Our quality management system includes ISO 9001 quality control procedures, incoming material inspection, production process monitoring, and finished product testing. Every rack system is carefully inspected through raw material testing, welding inspection, surface coating inspection, load-bearing testing, and dimensional accuracy checks before shipment.
We have a professional quality inspection team of 65 experienced QC specialists responsible for ensuring every product meets international standards and customer requirements.
With extensive international trade experience, Shibang has developed long-term cooperation with customers from North America, Europe, Southeast Asia, the Middle East, Africa, and South America. Our main markets include the United States, Germany, the United Kingdom, Australia, Saudi Arabia, Thailand, and Mexico.
Supported by a strong supply chain network of more than 1,200 reliable partners, we are capable of providing stable raw materials, efficient production capacity, and competitive pricing for global buyers. Our customers include warehouse operators, logistics companies, manufacturing enterprises, e-commerce businesses, distributors, system integrators, and construction contractors.
Shibang owns a professional R&D team with strong engineering capabilities, focusing on warehouse optimization, structural design, and customized storage solutions. We provide various customization options, including rack dimensions, loading capacity, colors, configurations, accessories, and complete warehouse planning solutions.
Every year, our R&D department develops approximately 120 new products to meet changing market demands and improve warehouse efficiency. Our team consists of 28 experienced R&D engineers specializing in product innovation, engineering design, and customized project development.
Driven by quality, innovation, and customer satisfaction, Guangdong Shibang Storage Rack Co., Ltd. is committed to becoming a trusted global partner for intelligent warehouse storage solutions.
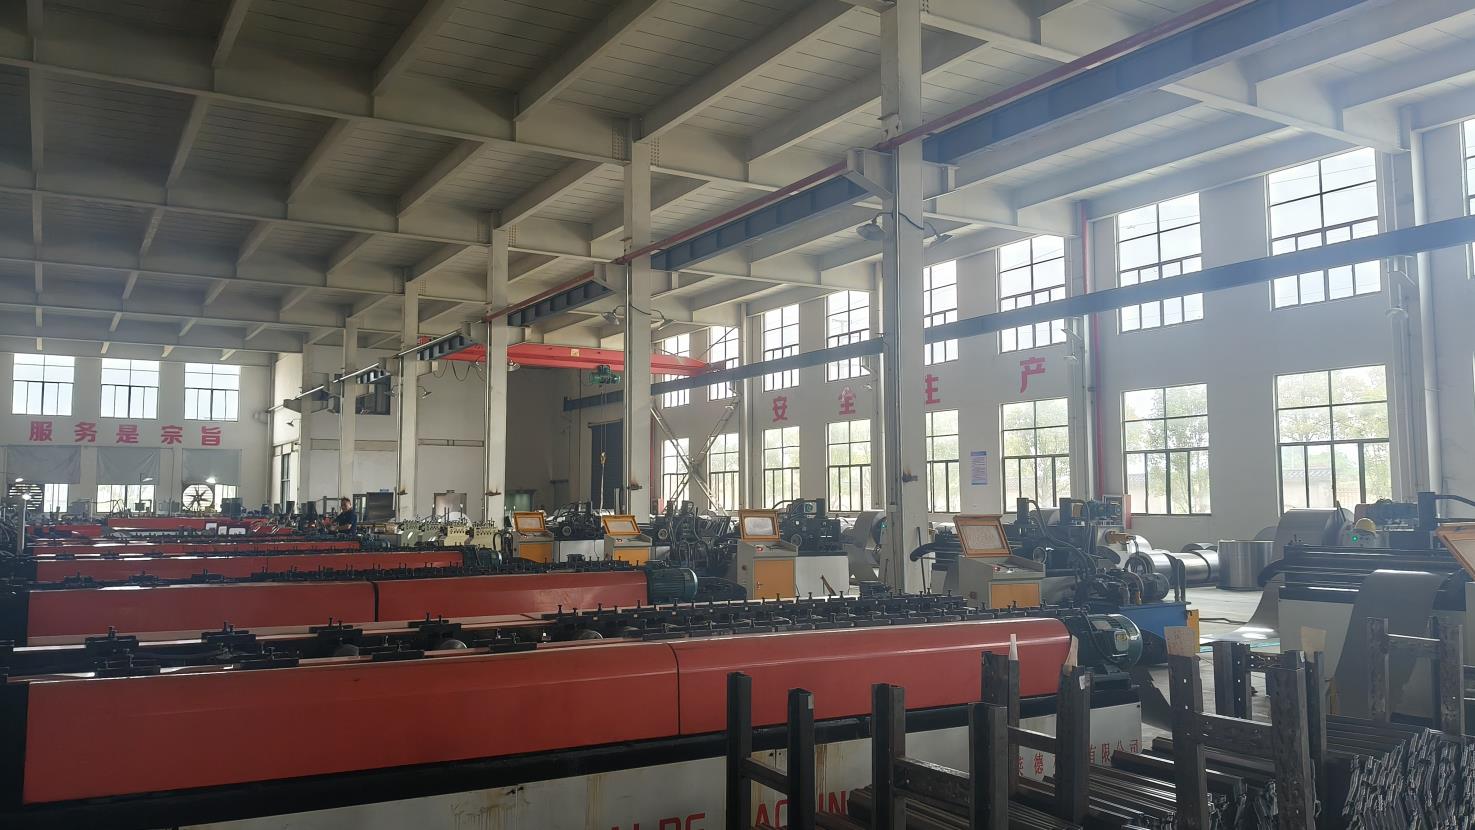
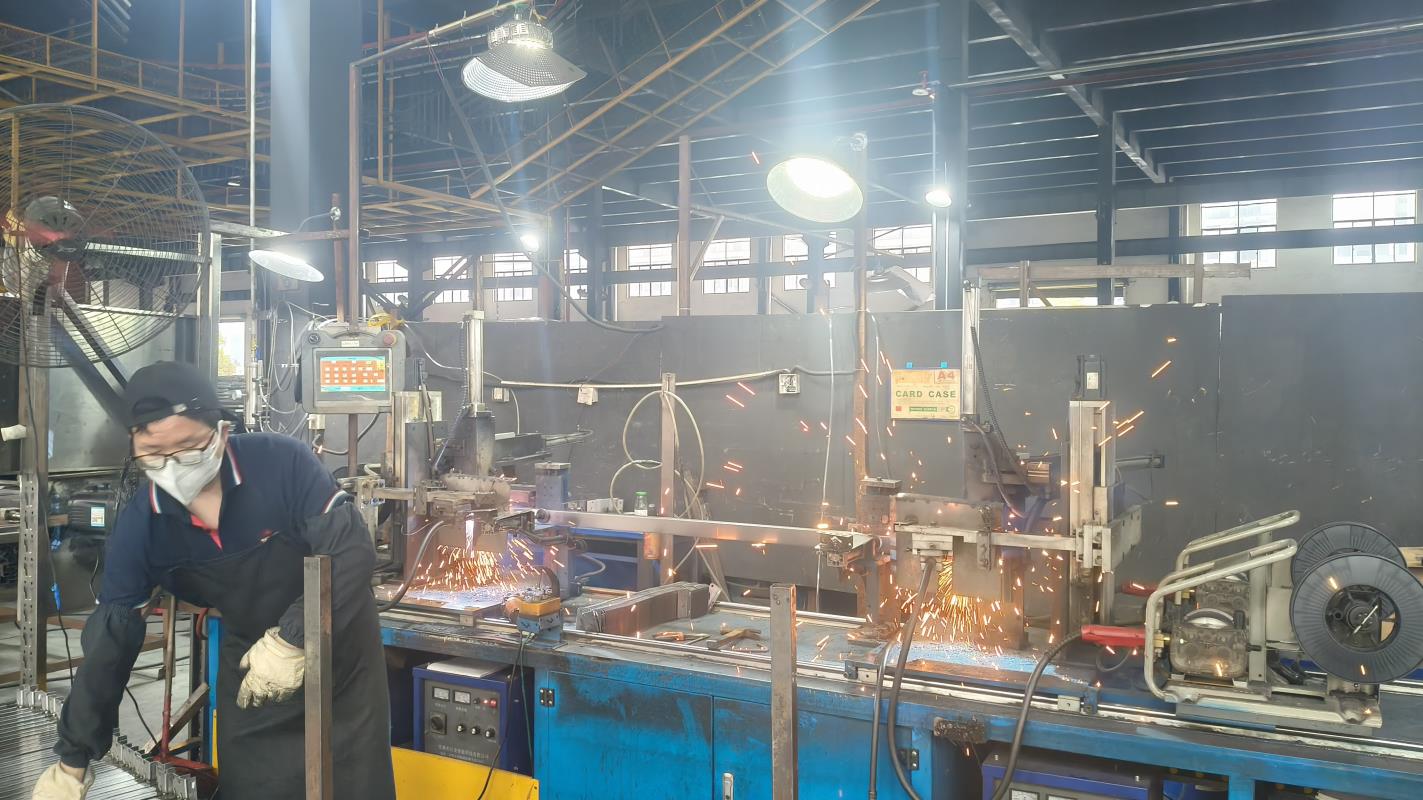
Our state-of-the-art facility is equipped with fully automated machinery and precision engineering tools, ensuring superior product consistency and structural durability across all manufacturing batches.
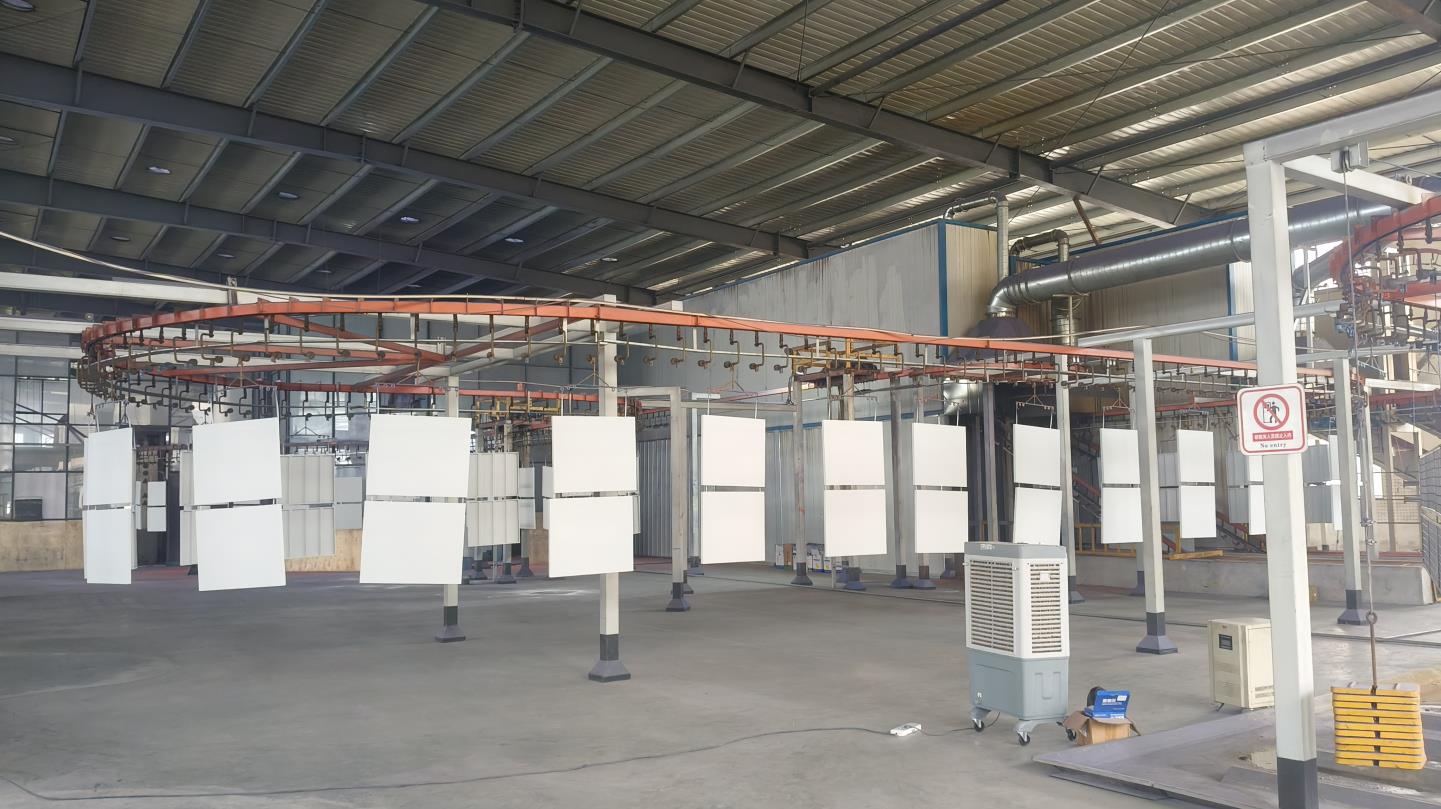
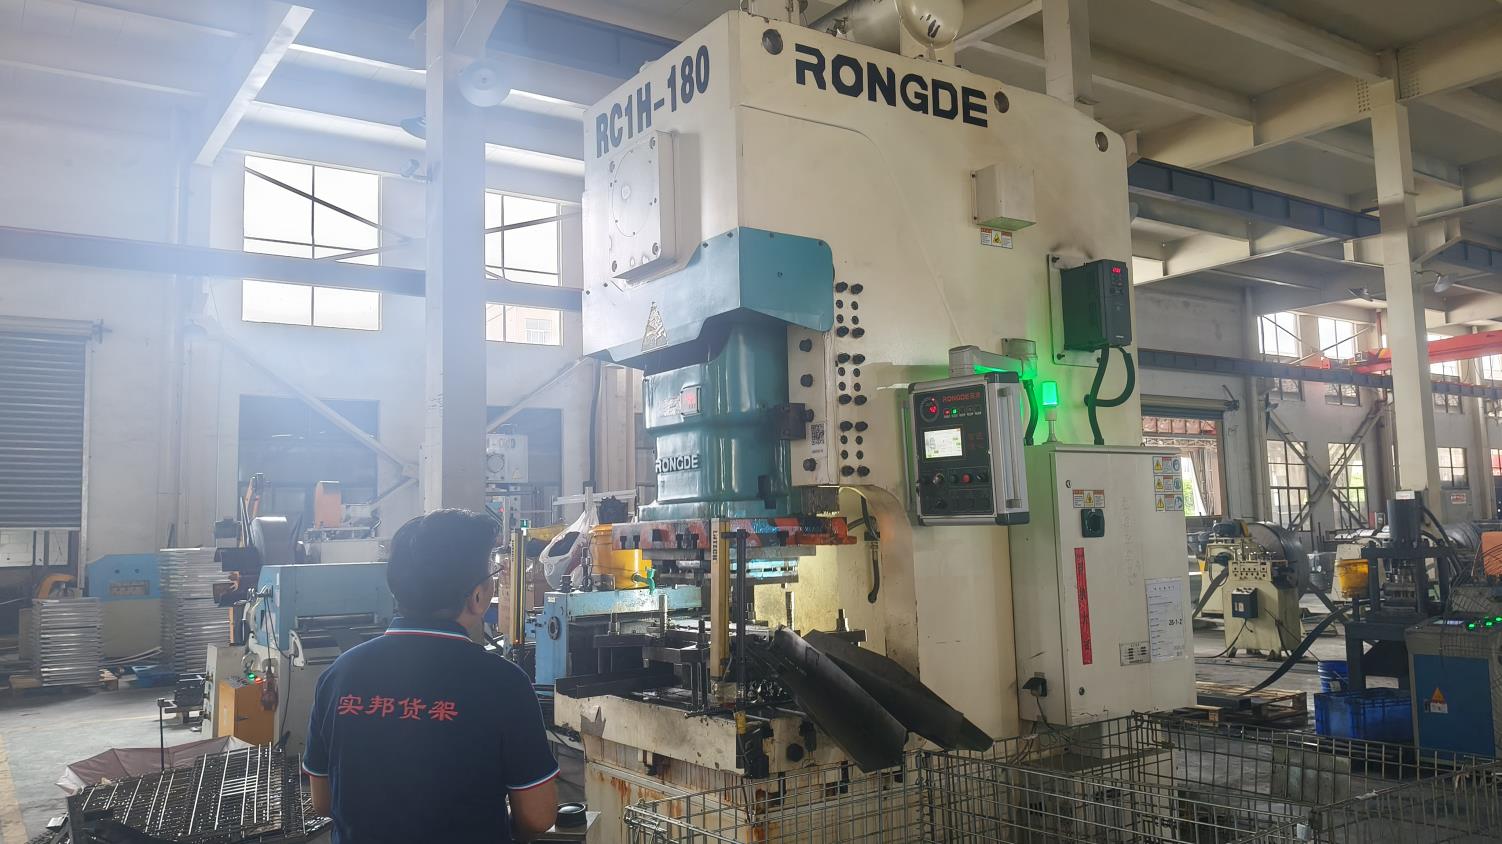
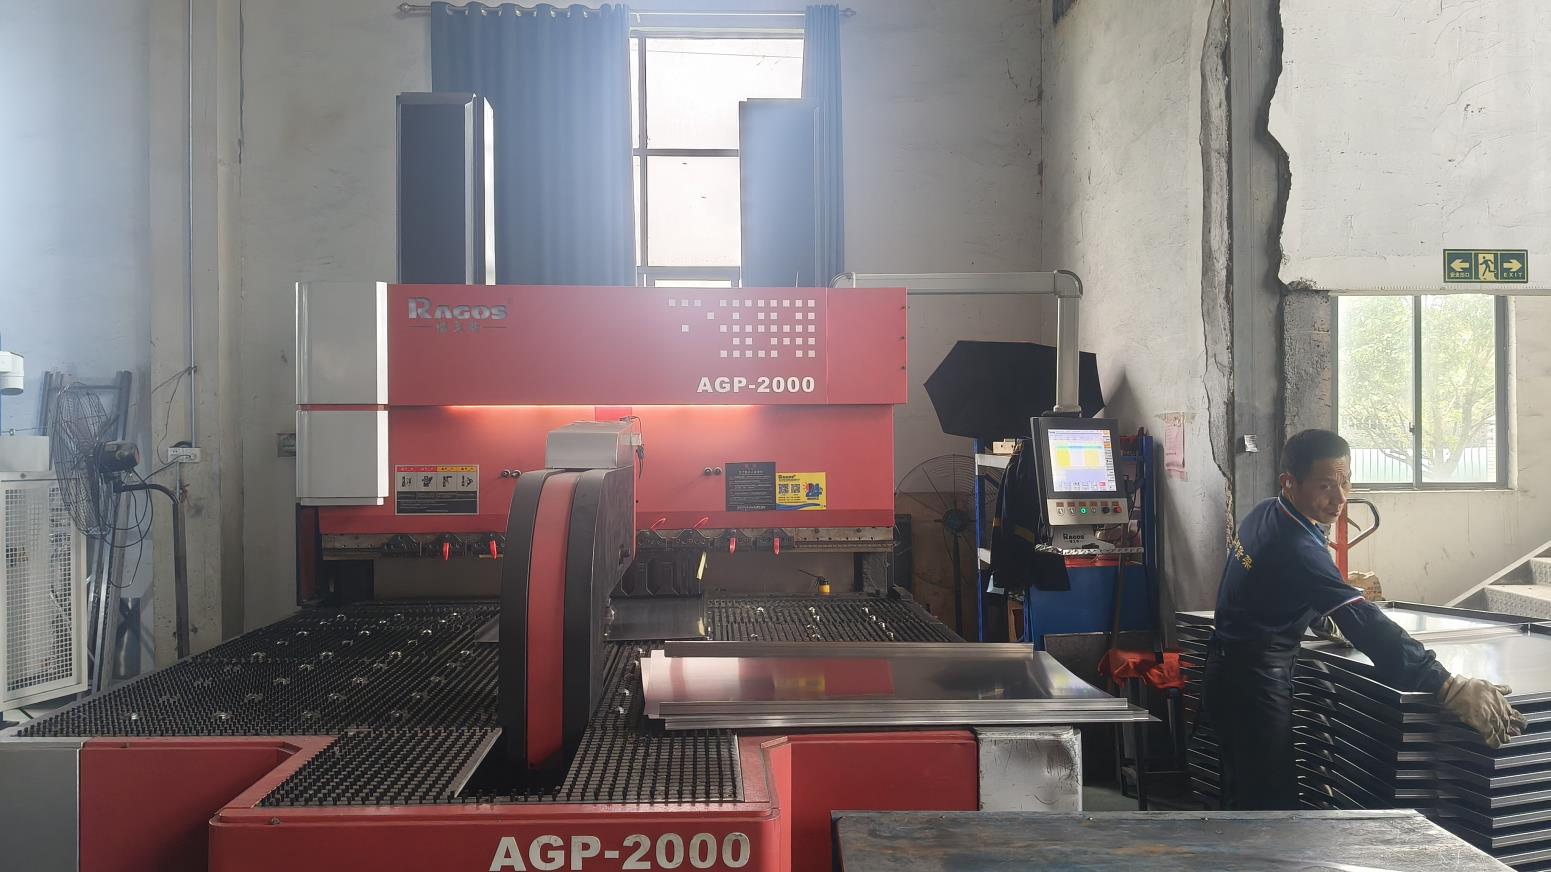
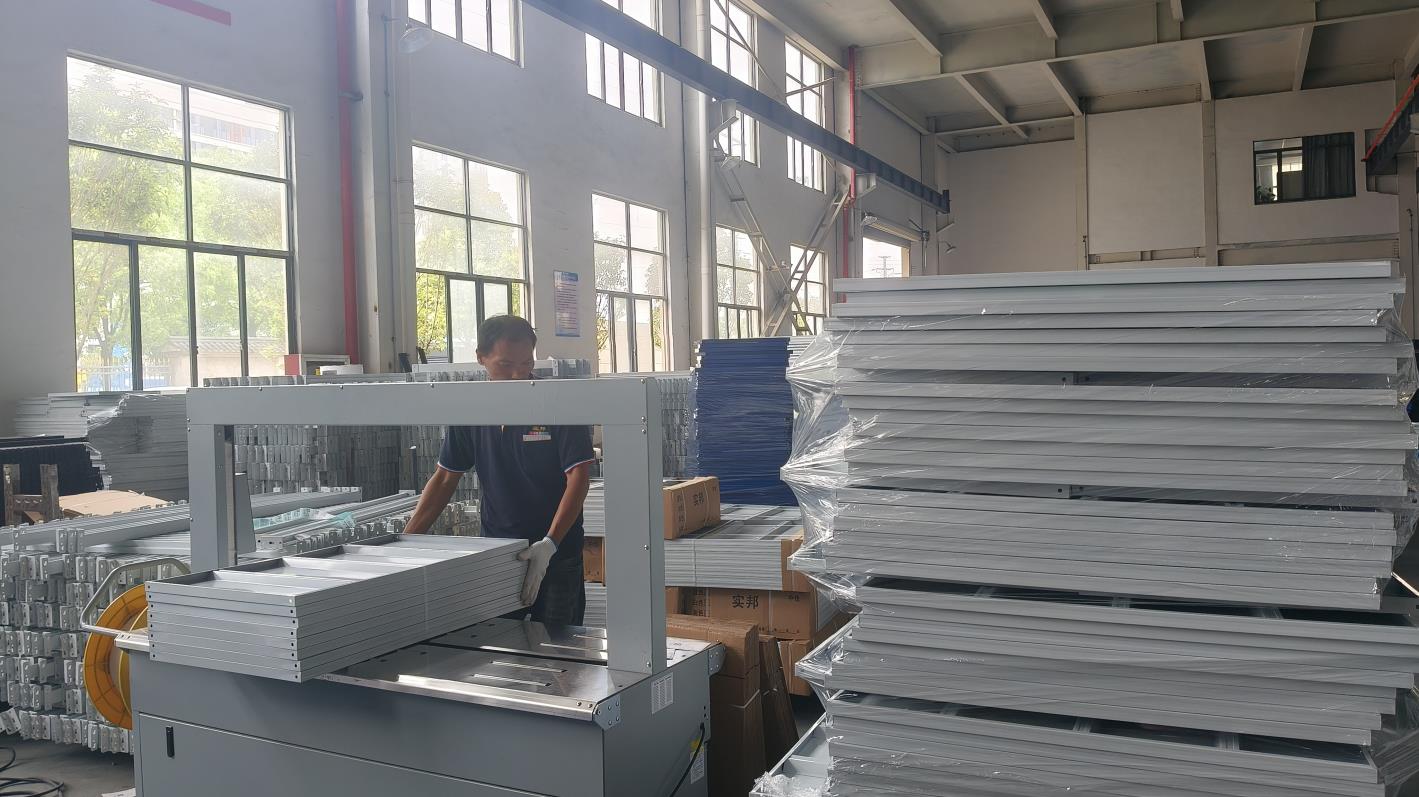
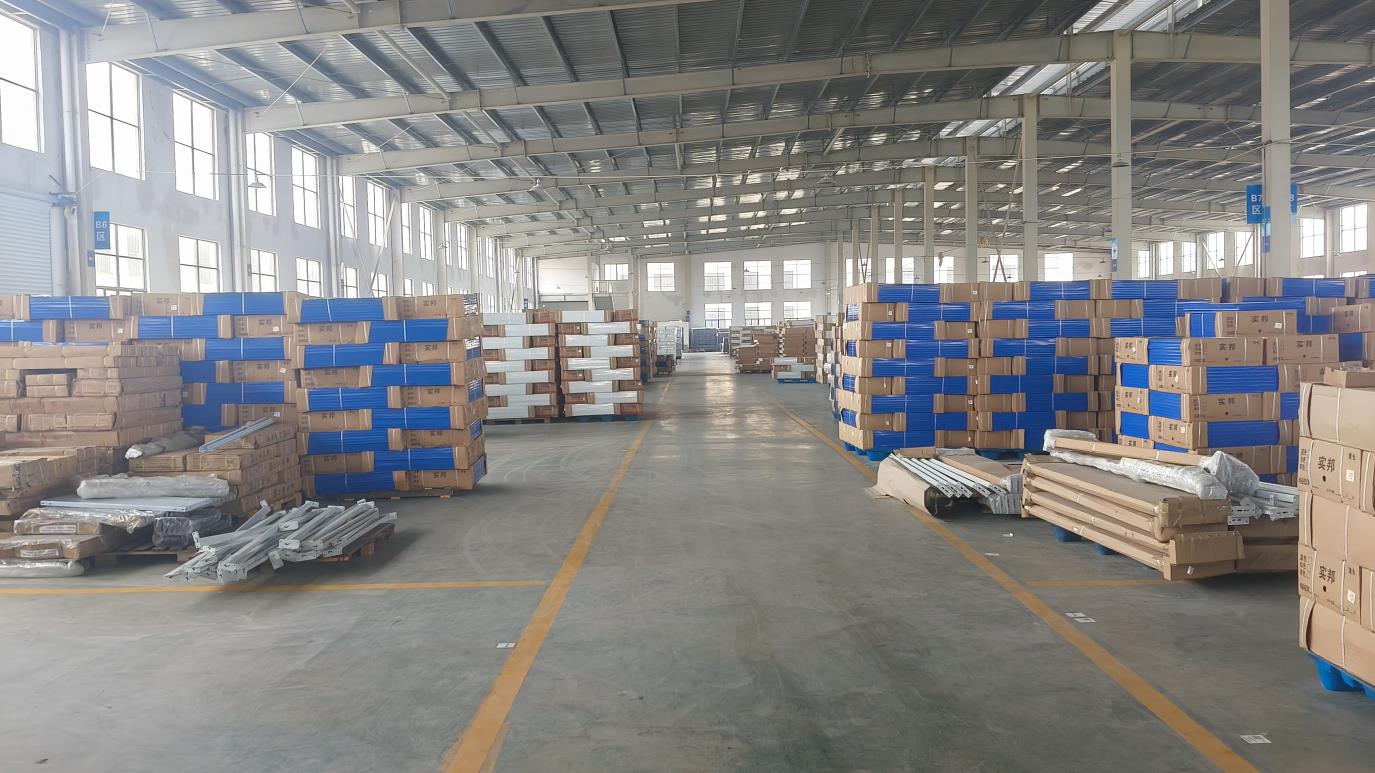
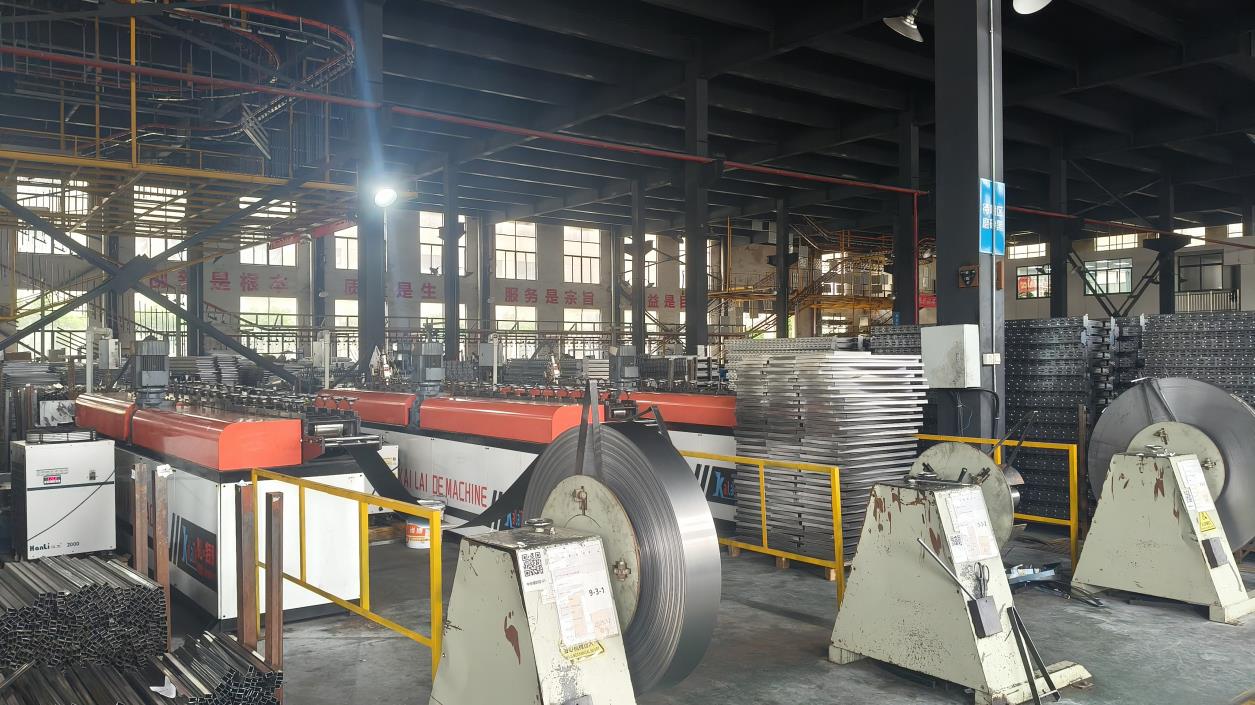
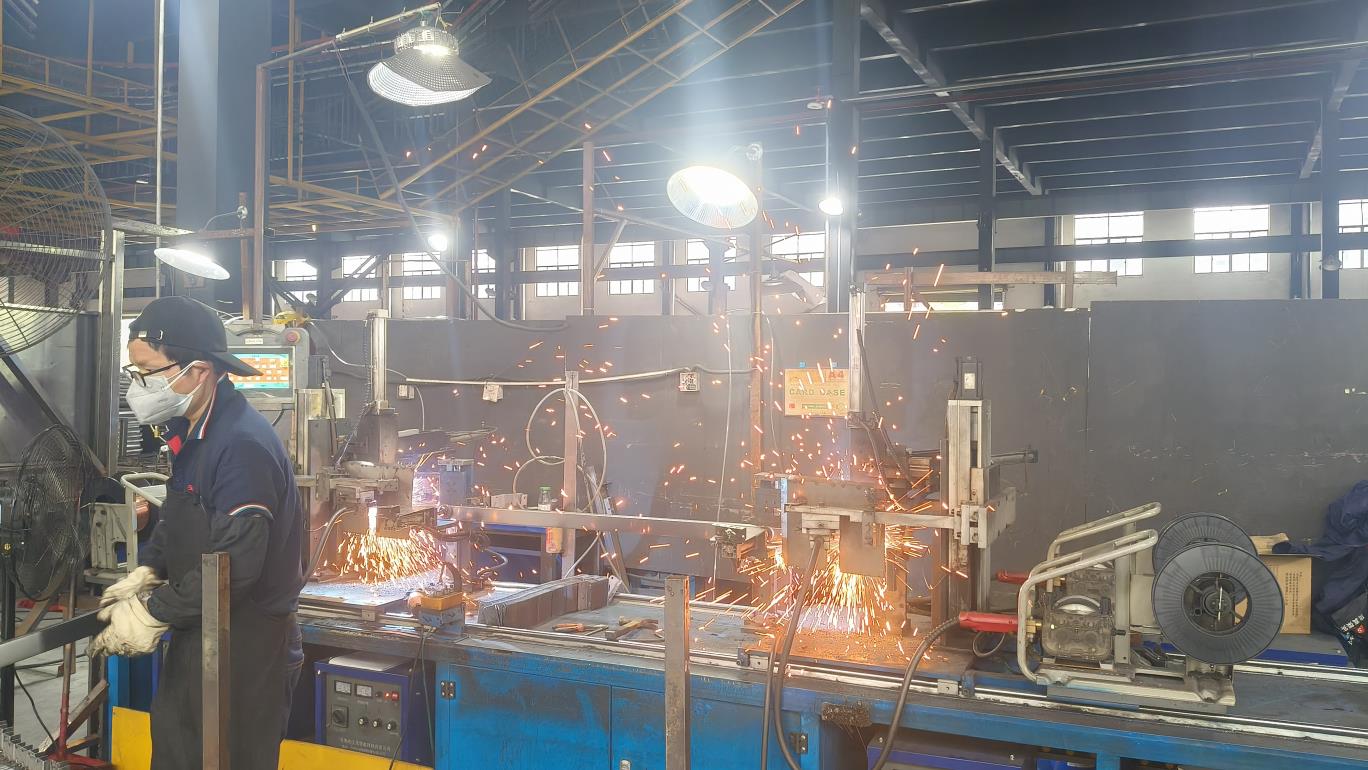
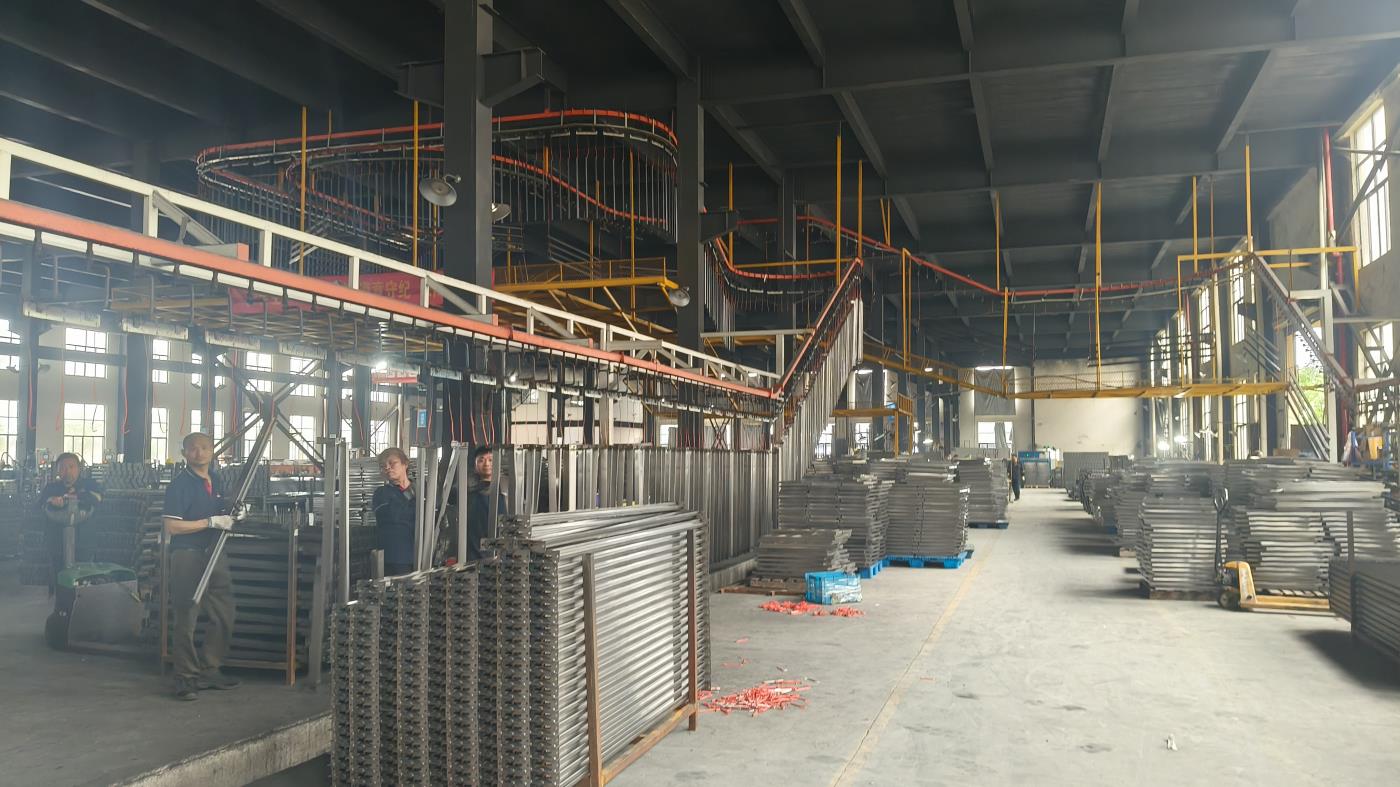
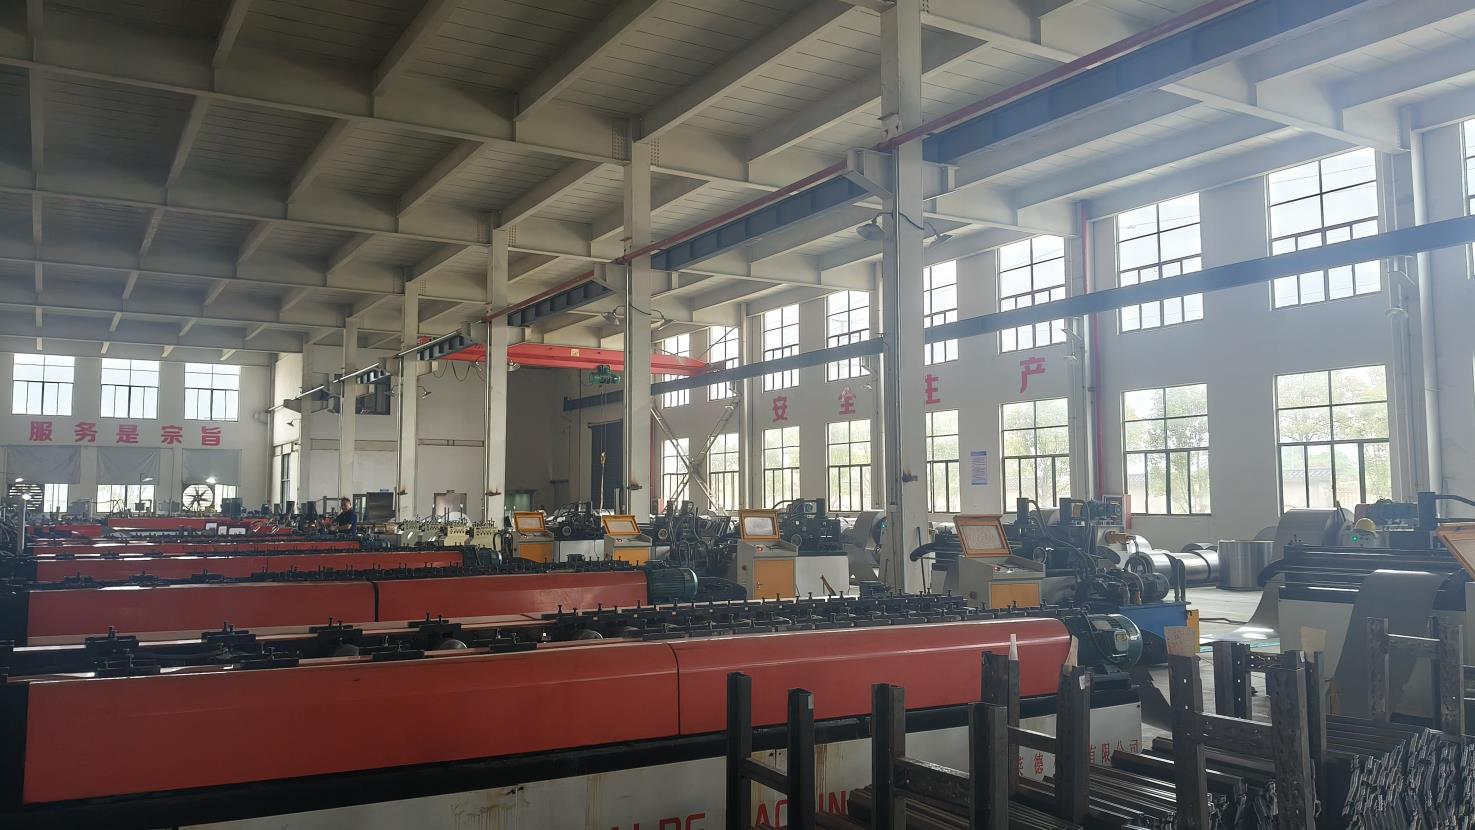
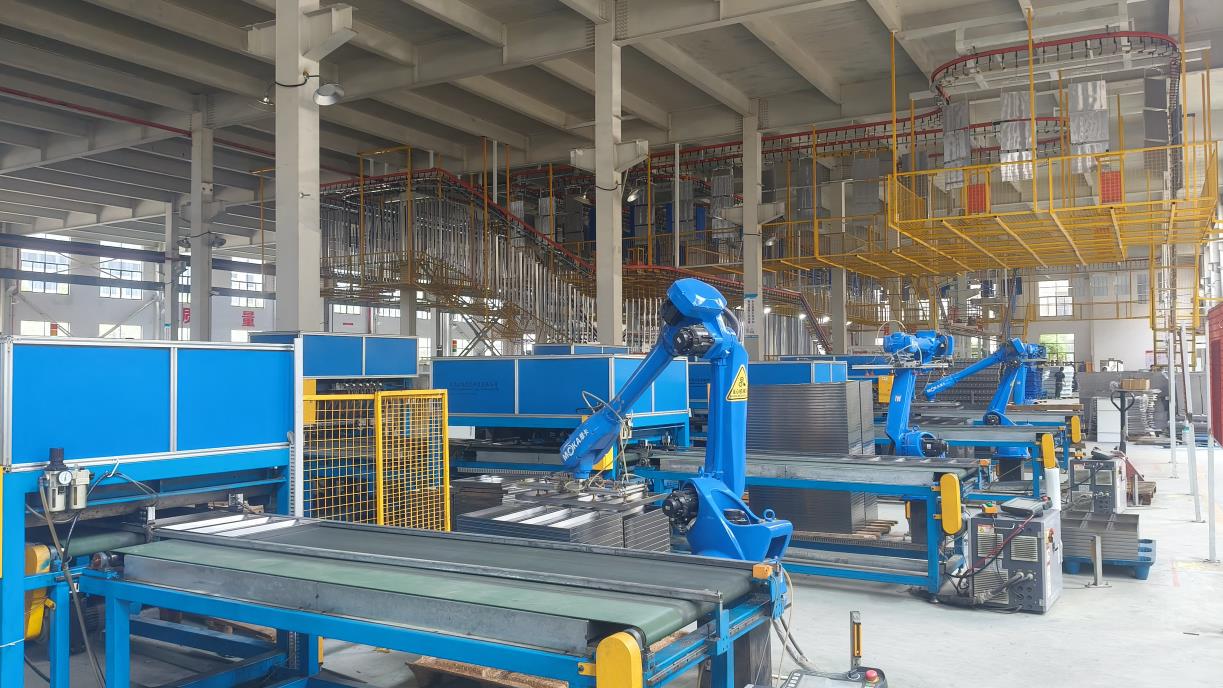
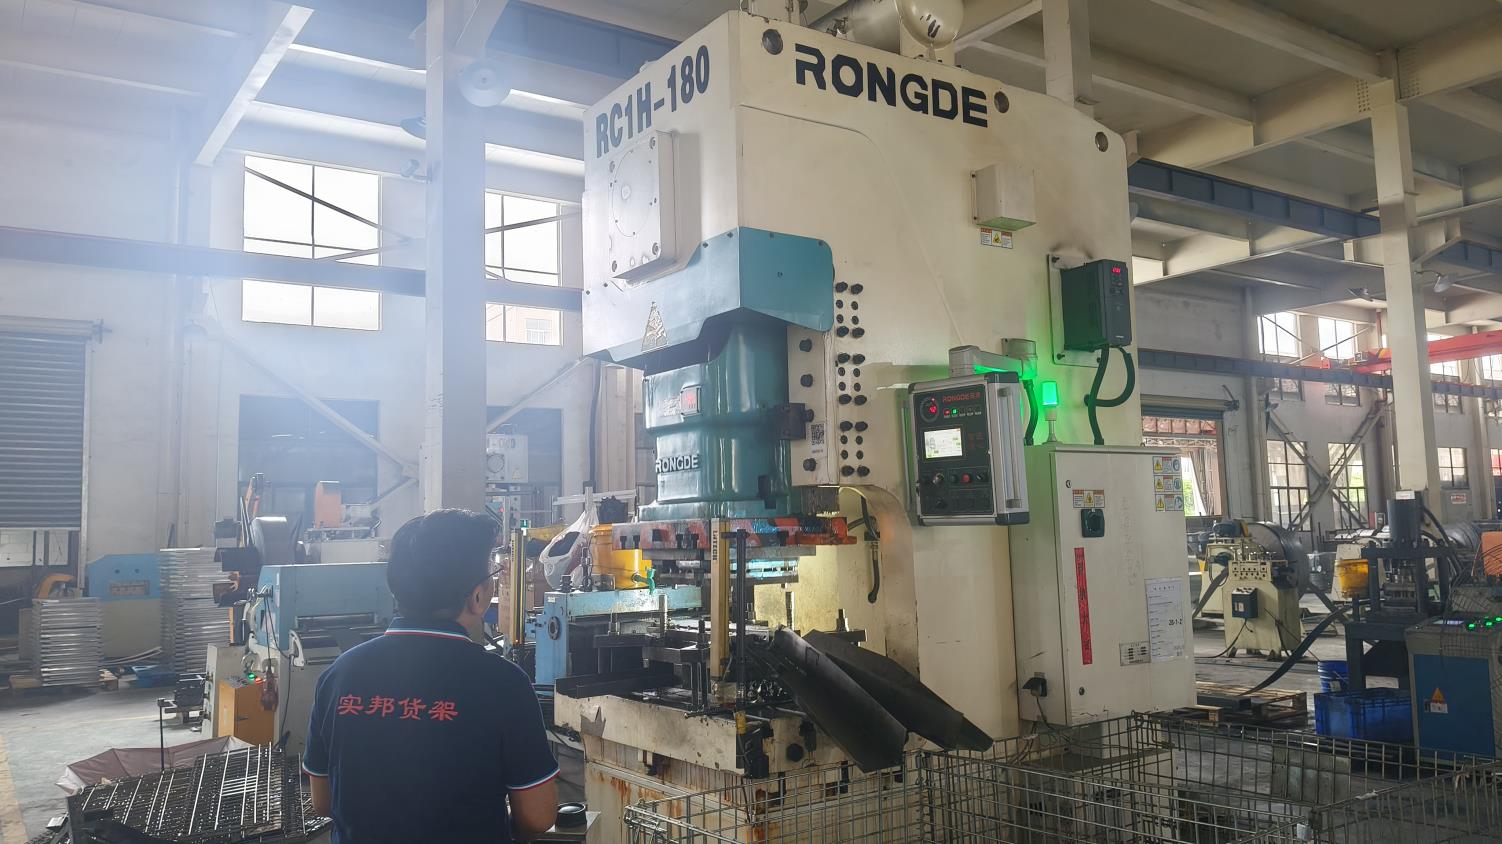
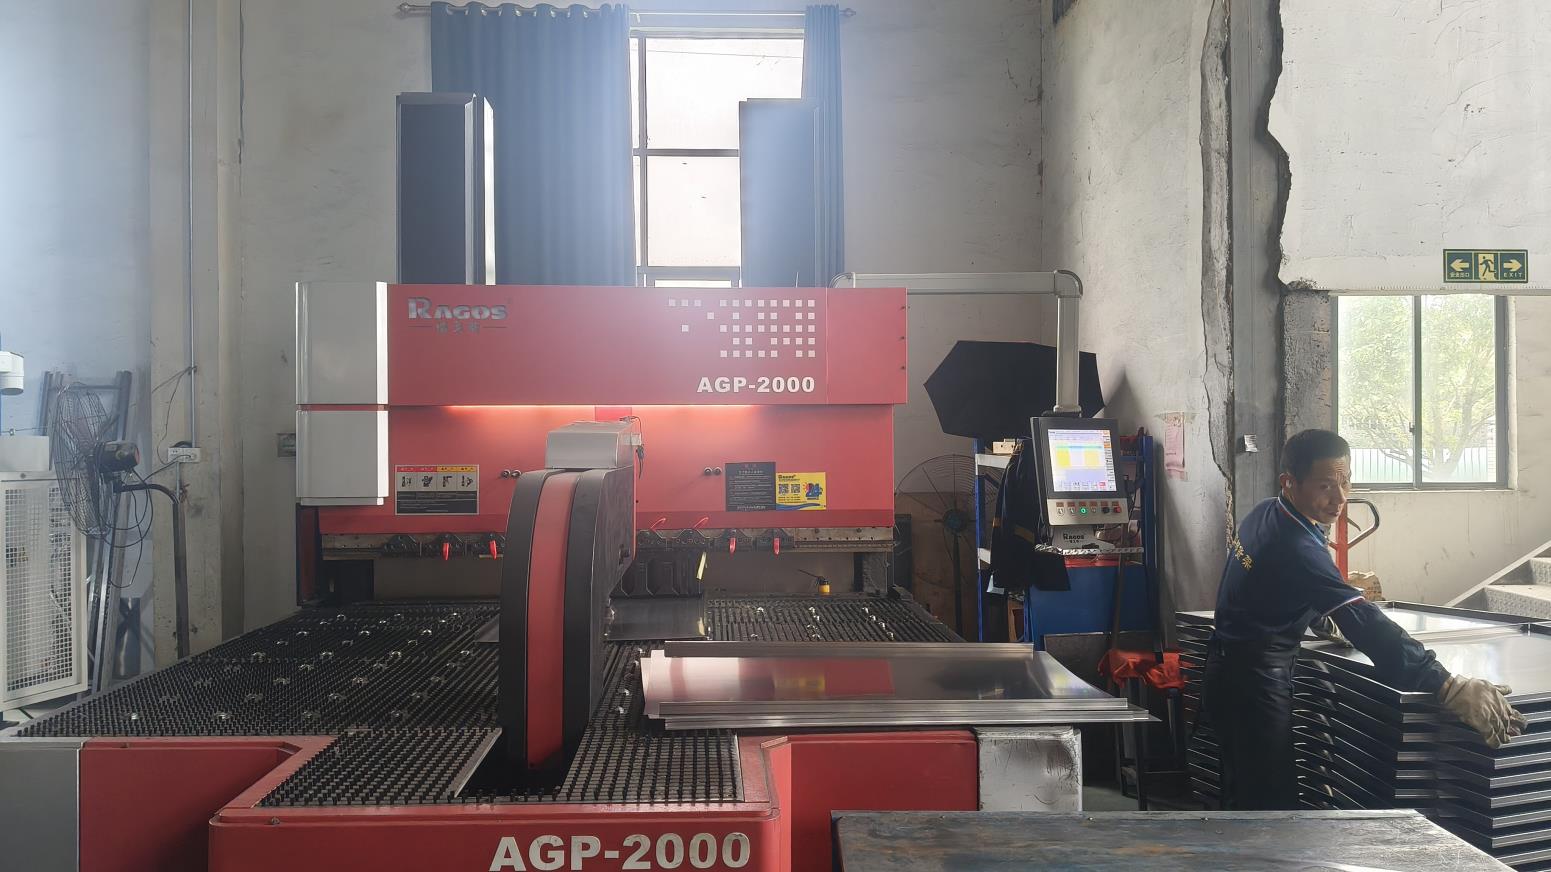
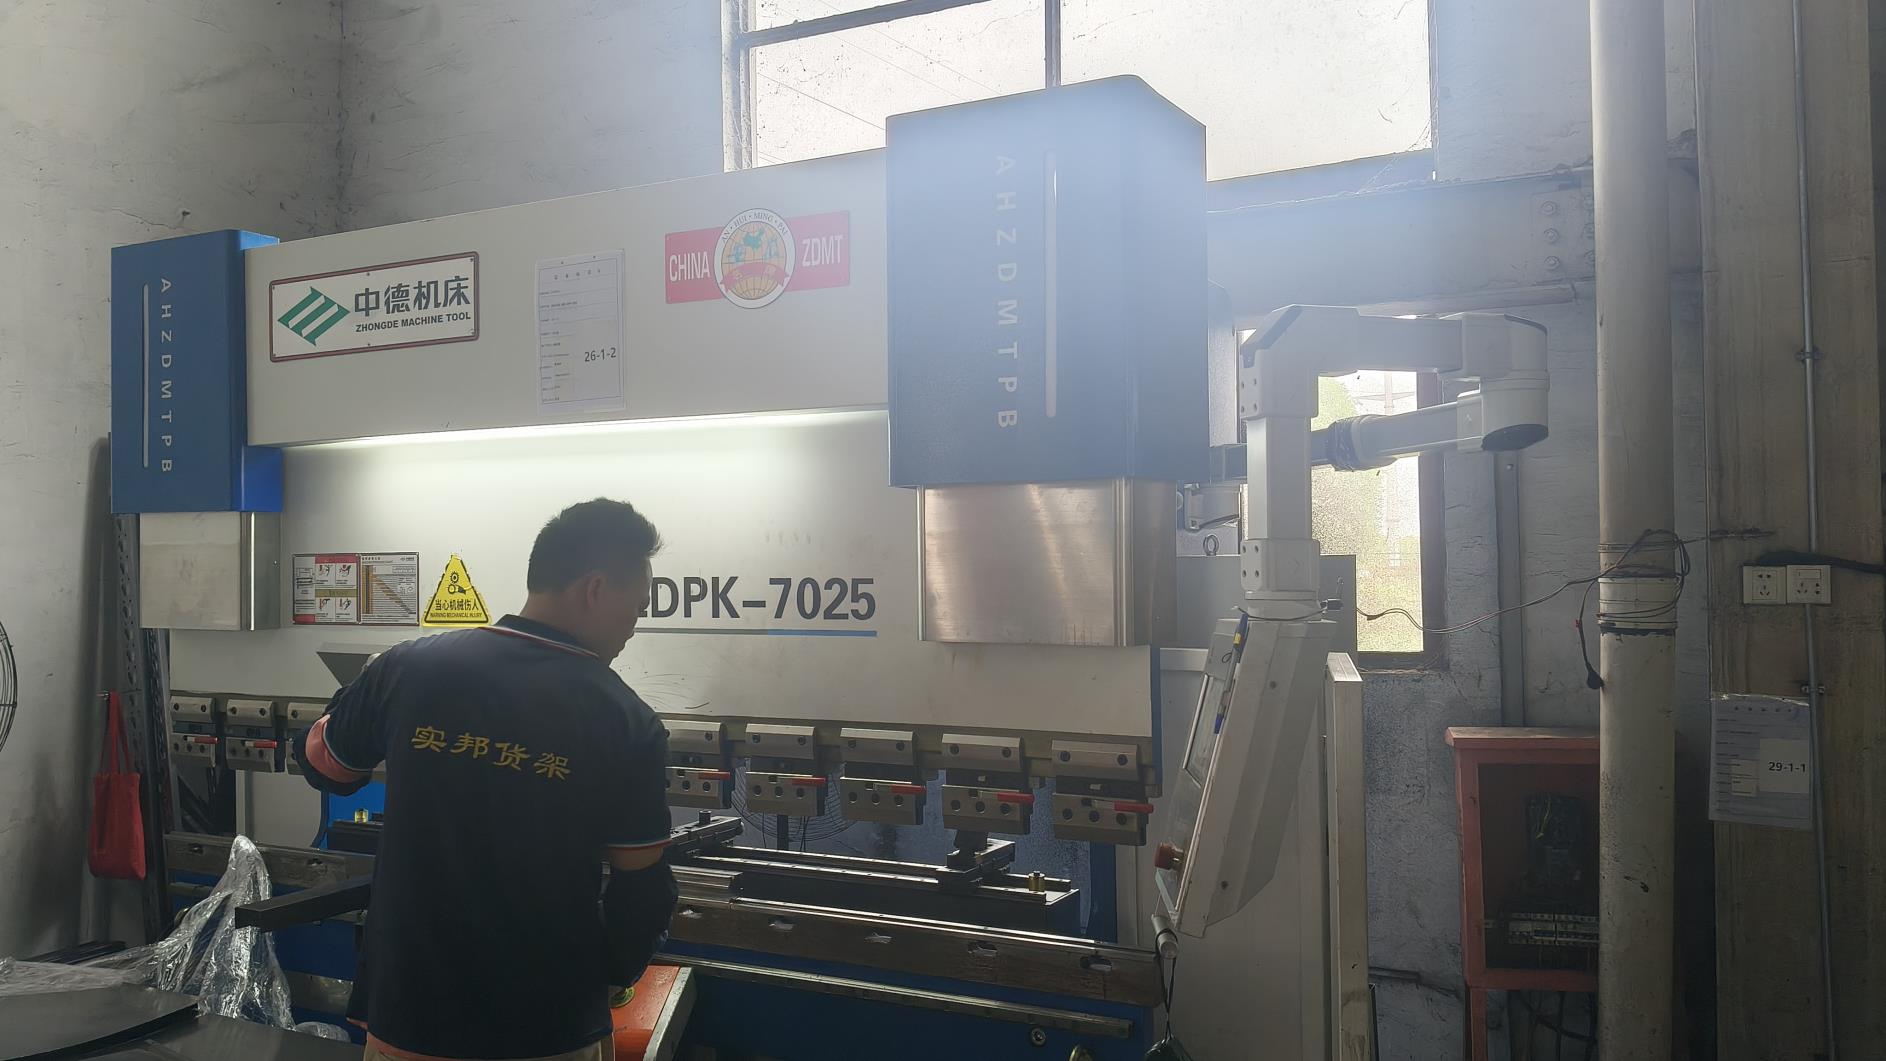
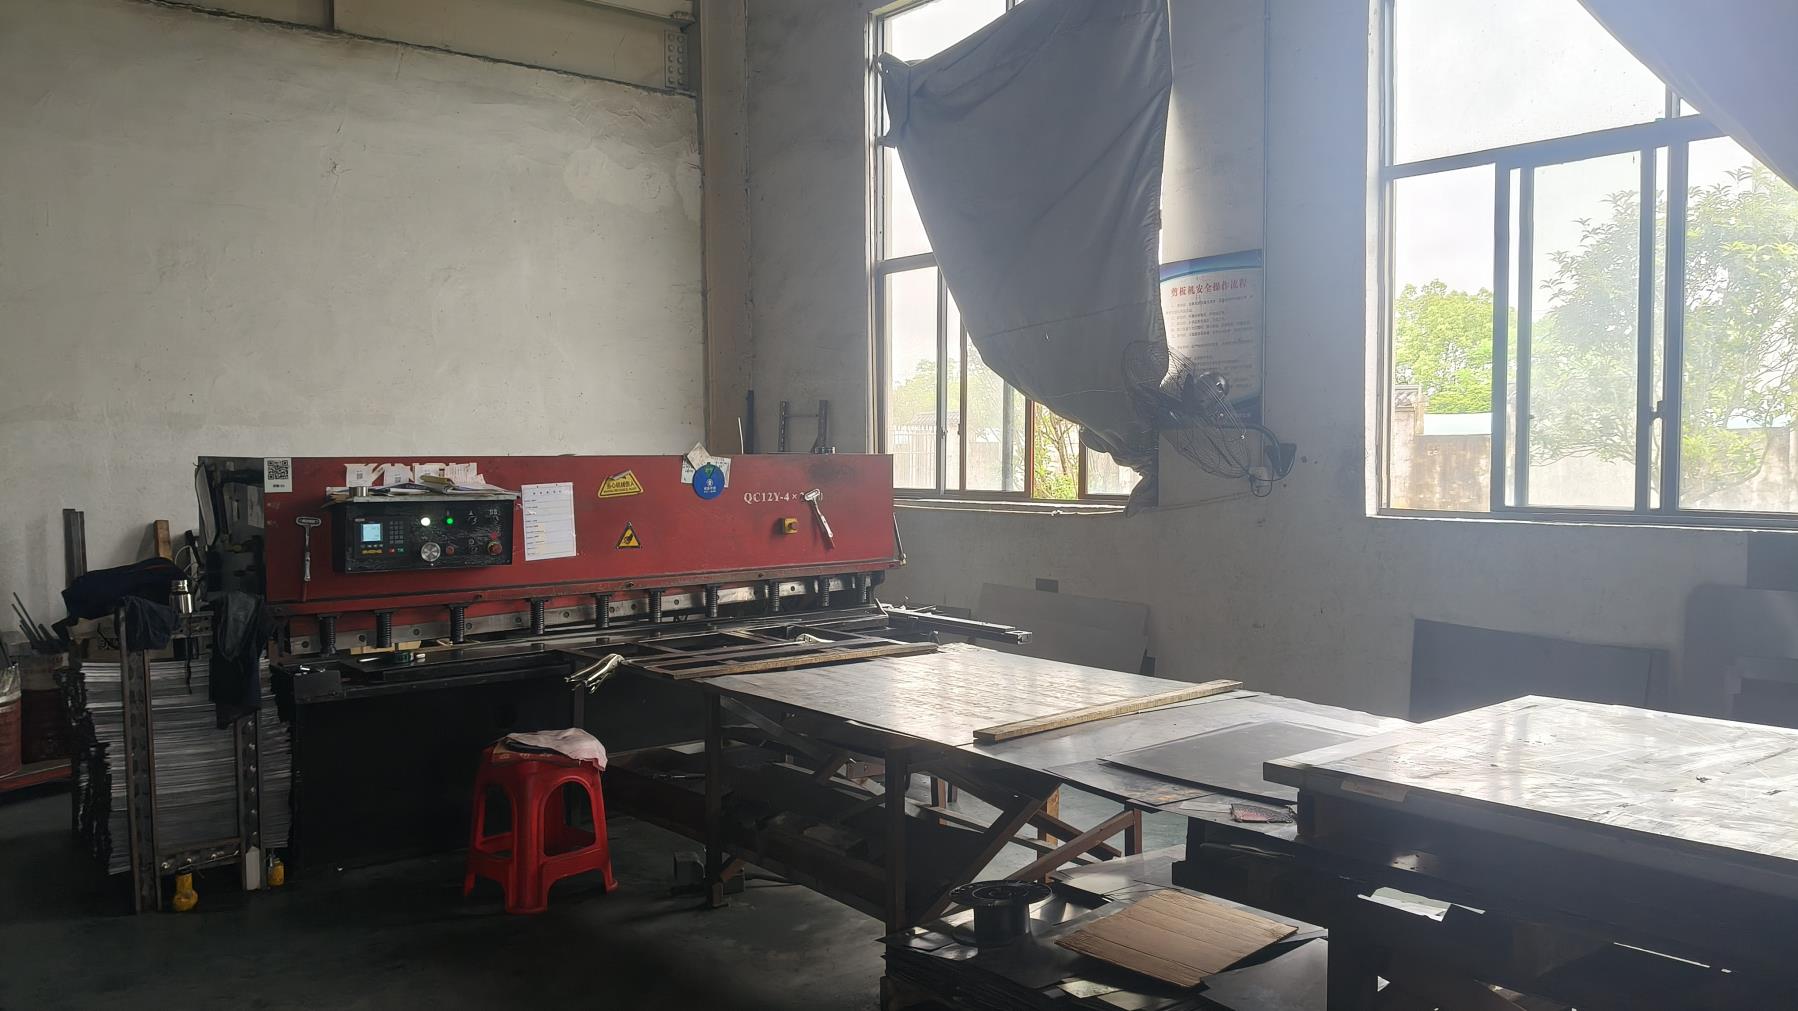
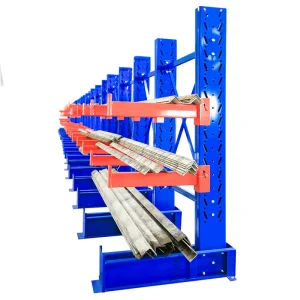
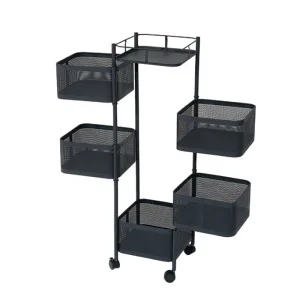
Explore our extensive catalog covering retail display racks, specialized fabric roll holders, multi-tier mezzanine shelving, and corrosion-resistant industrial storage units.
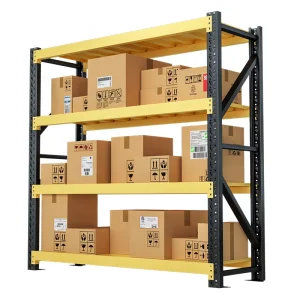
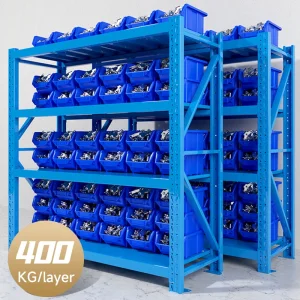
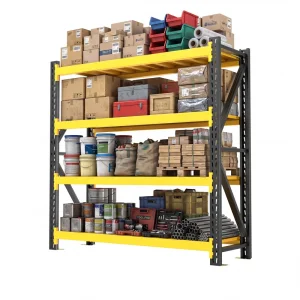
The next decade of warehouse storage engineering will be defined by smart integration, IoT-enabled weight sensors, anti-seismic structural optimizations, and eco-friendly powder coating technologies. At Guangdong Shibang Storage Rack Co., Ltd., our R&D roadmap focuses on developing modular, tool-free assembly systems that reduce deployment time while maximizing vertical clearance efficiency.
By leveraging advanced FEA (Finite Element Analysis) simulation tools during the design phase, our engineers accurately predict stress distribution and load deflection under extreme operating conditions. This commitment to technical excellence ensures that global B2B buyers receive future-proof infrastructure capable of supporting autonomous mobile robots (AMRs) and automated storage and retrieval systems (AS/RS).
Our heavy duty industrial racks typically offer adjustable load capacities ranging from 400kg, 600kg, 800kg, up to 1500kg per layer, customized precisely based on your inventory weight and pallet dimensions.
Yes, all our racking systems are manufactured under strict ISO 9001 quality management procedures and hold CE certifications, ensuring compliance with global structural safety and load-bearing regulations.
Absolutely. Our professional R&D team of 28 engineers provides full warehouse planning solutions, tailoring rack dimensions, tier heights, colors, and specific configurations to meet your precise layout requirements.
We have extensive export experience spanning North America, Europe, Southeast Asia, the Middle East, Africa, and South America, maintaining long-term partnerships in the US, Germany, UK, Australia, Saudi Arabia, Thailand, and Mexico.
 Shibang Storage Rack